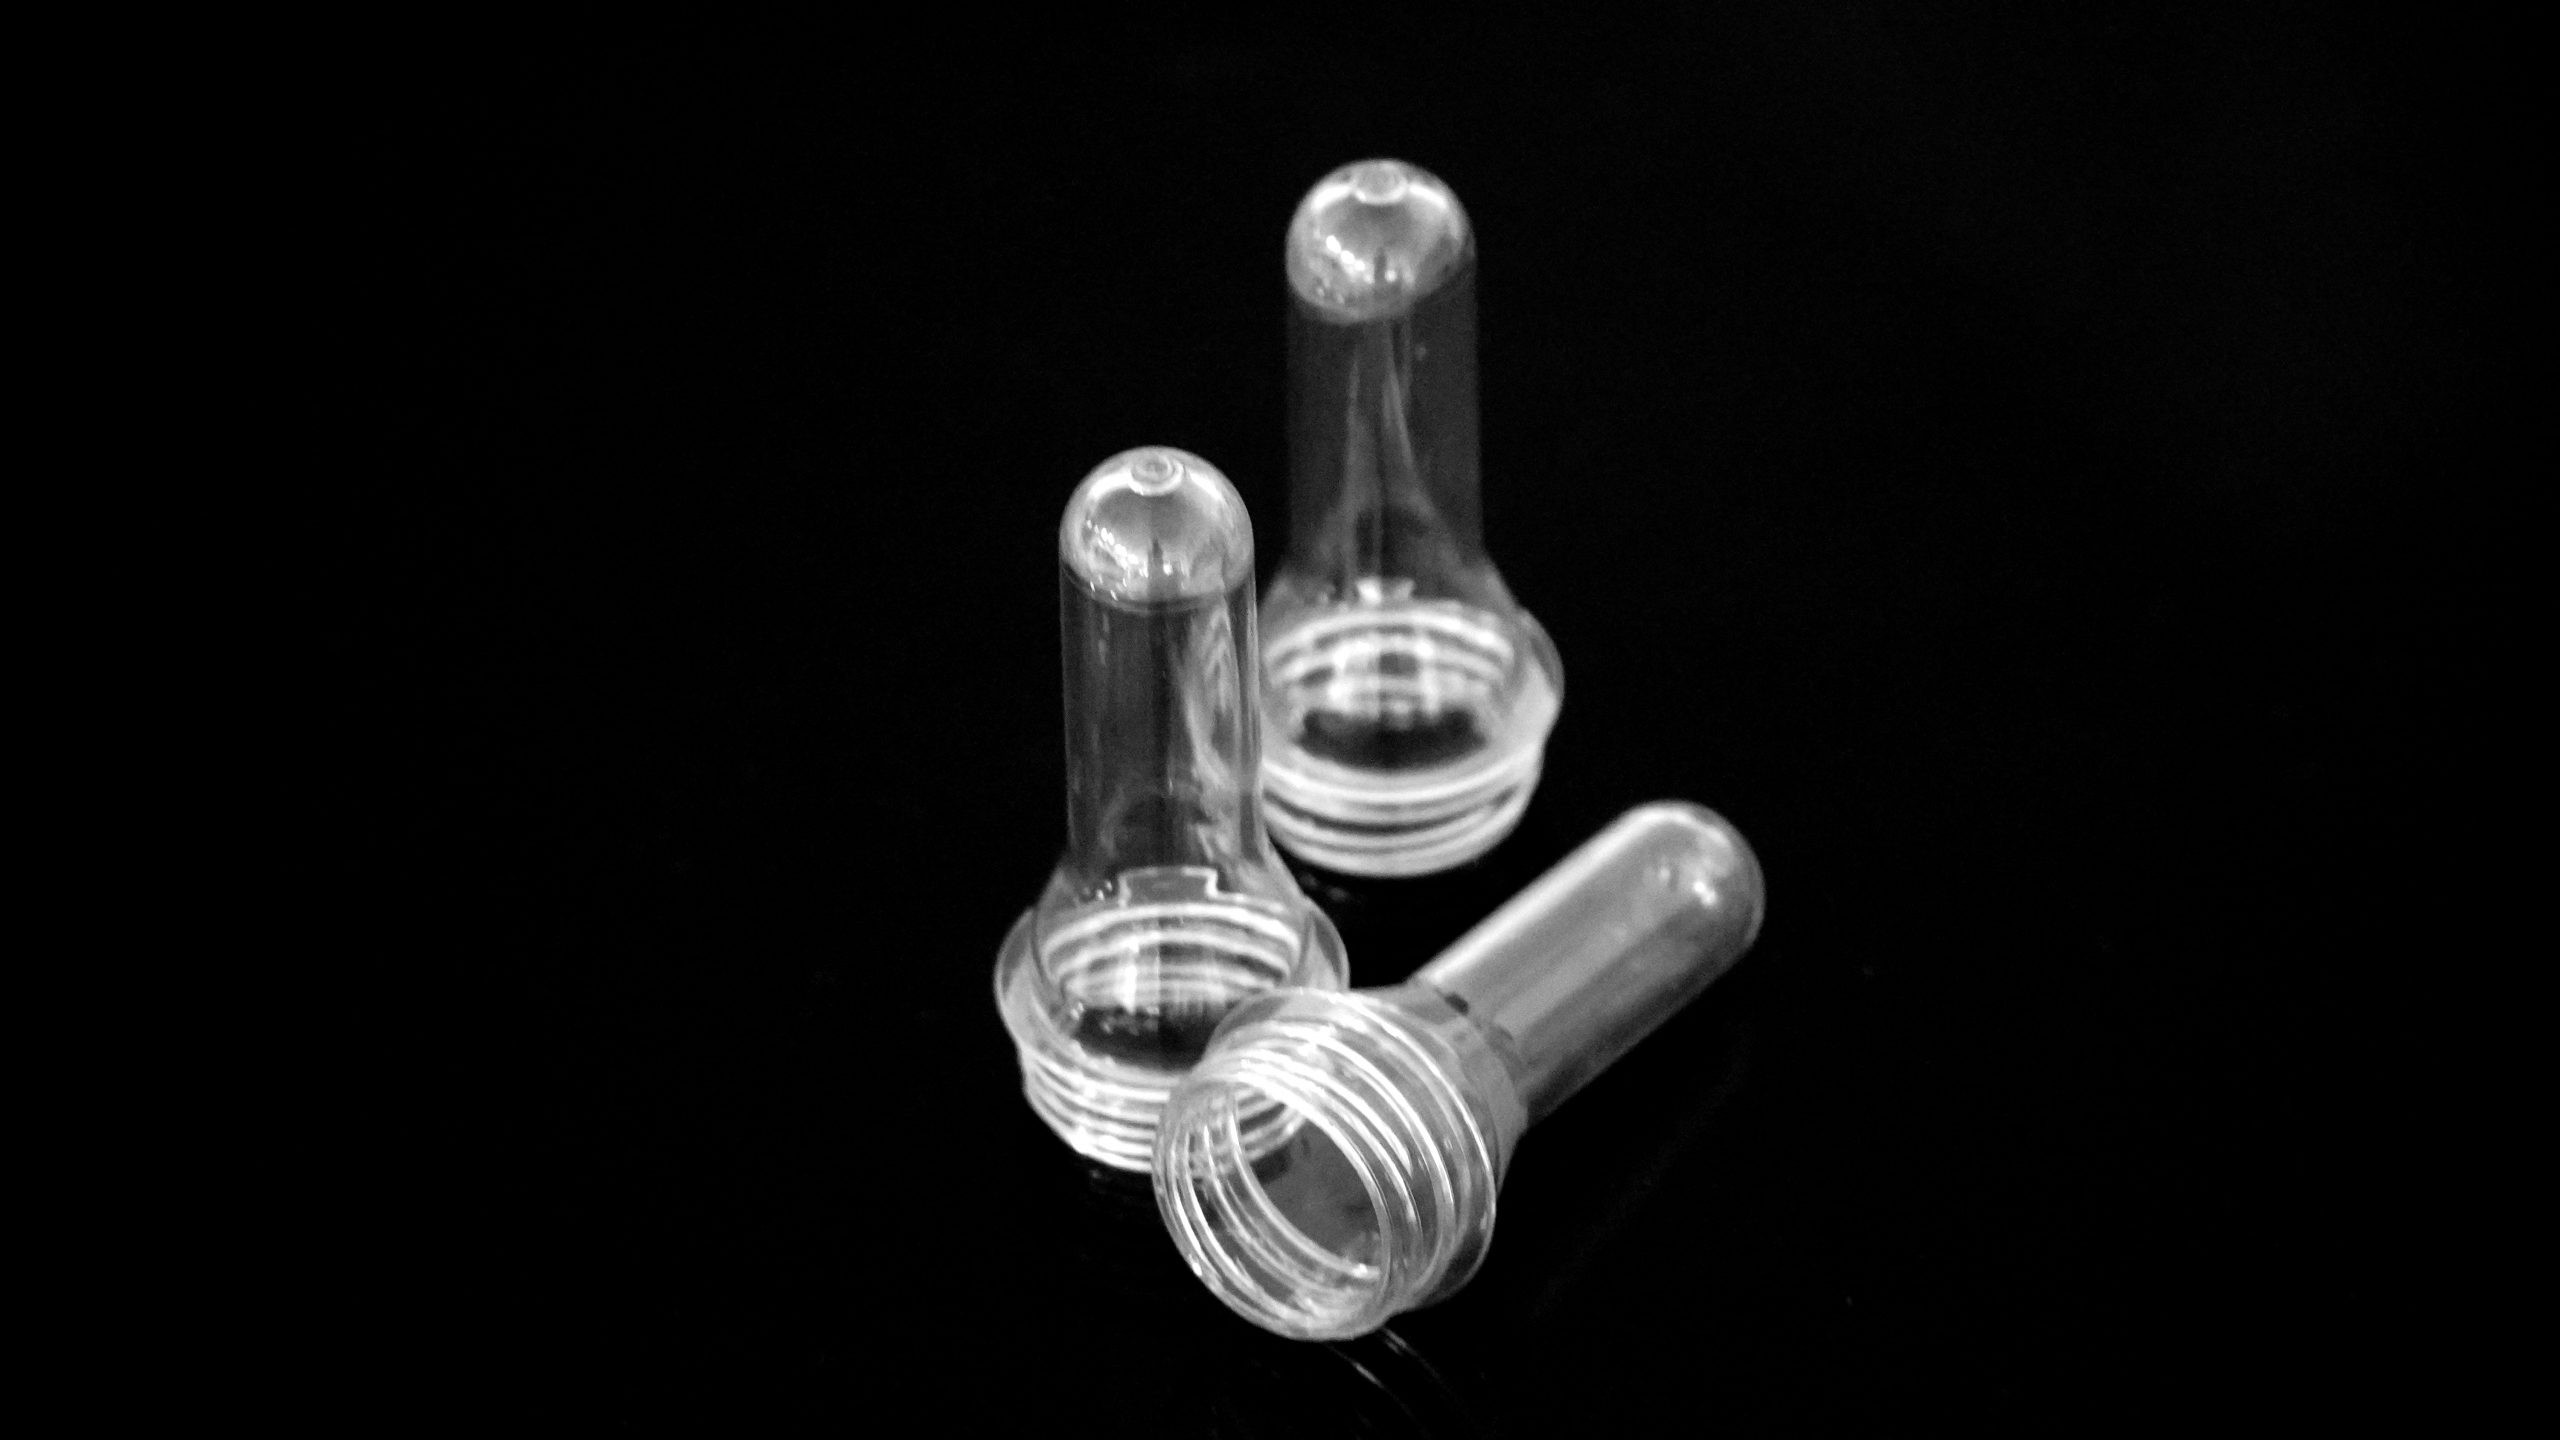
PET Preform Injection Molding Machine: DKM’s 12-Second Cycle
Focus on reducing your overall production costs. The robust clamping system and efficient design provide consistent.
Understanding the PET Preform Challenge
Producers of water and beverage packaging face a recurring set of operational pressures: long equipment lead times, high per-unit production costs, slow molding cycles, and inconsistent output across high-cavity molds. For PET preform manufacturing specifically, the stakes are higher because preform producers need large melting capacity, high-efficiency injection, and dependable multi-cavity consistency to meet market demand windows. Within this context, DKM Machinery and SINO MOULD have built a combined machine-and-mold capability specifically engineered to address these pain points.
DKM-PET III: A Preform-Dedicated Injection Molding Machine
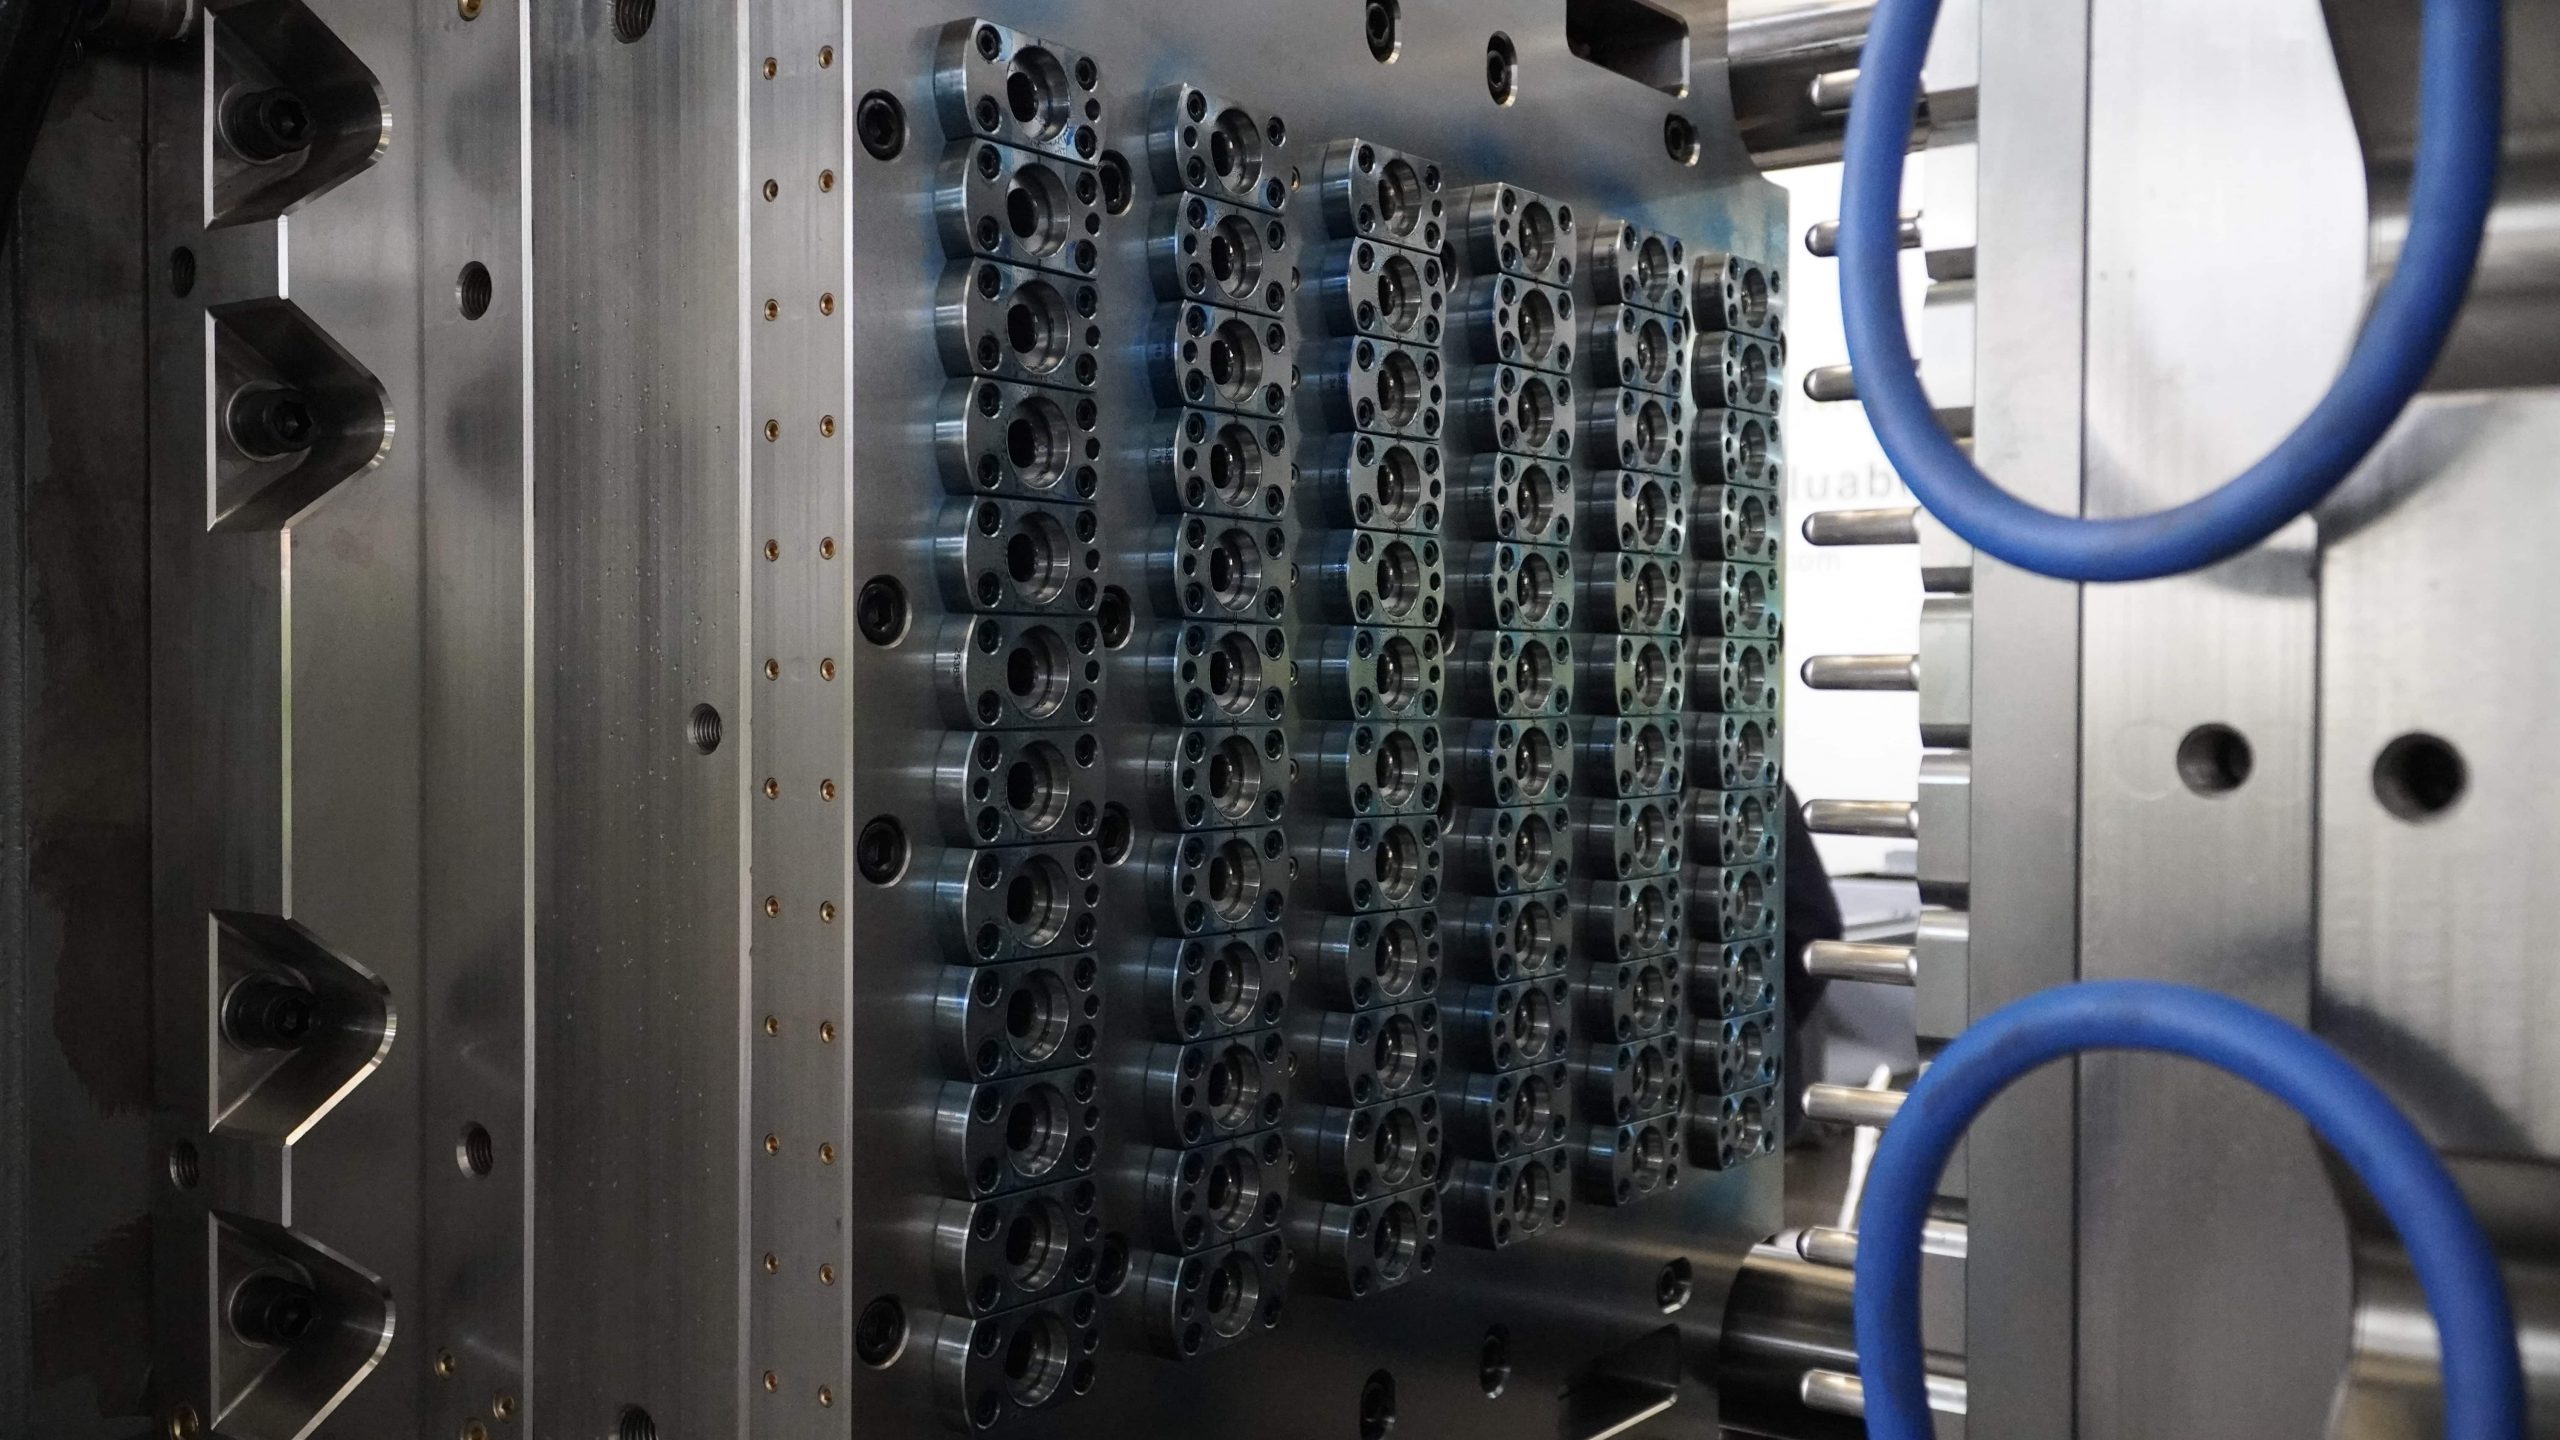
The DKM-PET III Preform-Dedicated Injection Molding Machine is offered across four models — DKM-350 PET III, DKM-450 PET III, DKM-550 PET III, and DKM-650 PET III — each paired with a specific cavity range: the DKM-350 PET III with 48-cavity lines, the DKM-450 PET III with 72-cavity lines, the DKM-550 PET III with 96-cavity (and in some configurations 144/168-cavity) molds, and the DKM-650 PET III with 144-cavity production lines.
What differentiates this series is its approach to cycle compression and repeatability. The machine uses a standard electric accumulator with synchronized plasticizing combined with post-mold cooling technology to shorten molding cycles, while nano far-infrared heating rings reduce production energy consumption. Perhaps most notably, the optimized machine frame structure delivers an injection repeat accuracy of ≤0.5‰ — a tolerance level that directly supports stable multi-cavity preform production, where even minor shot-weight variation across dozens of cavities can translate into scrap and rework.
Demonstrated Cycle Performance
Numbers matter more than claims in this industry, and DKM’s documented results speak to real production conditions:
- A 144-cavity preform mold running on the DKM-650 PET III achieves a 12.8-second cycle time, producing an 11g, 29mm-neck preform.
- A 168-cavity mold on the DKM-550 PET III, with an 11g product weight and BPF 26/21 neck, runs an 11-second cycle.
- A 72-cavity standard line paired with the PET 450 achieves a 12-second cycle for a 12g, 28mm preform.
- A 48-cavity standard line with the PET 350 completes a 16-second cycle for the same 12g, 28mm preform specification.
- In a separate 72-cavity configuration equipped with an out-mold cooling system, a 13.5g, 28mm-neck preform is produced at a 12-second cycle.
- Continued process refinement brought the molding cycle for a 26g preform down to 12 seconds, supported by mold component tolerance held to 0.005mm.
These figures illustrate a consistent engineering pattern: as cavity count rises, DKM’s accumulator-and-cooling architecture is designed to hold cycle times within a tight, predictable band rather than letting them scale unfavorably with cavity density.
Turnkey PET Preform Production Lines
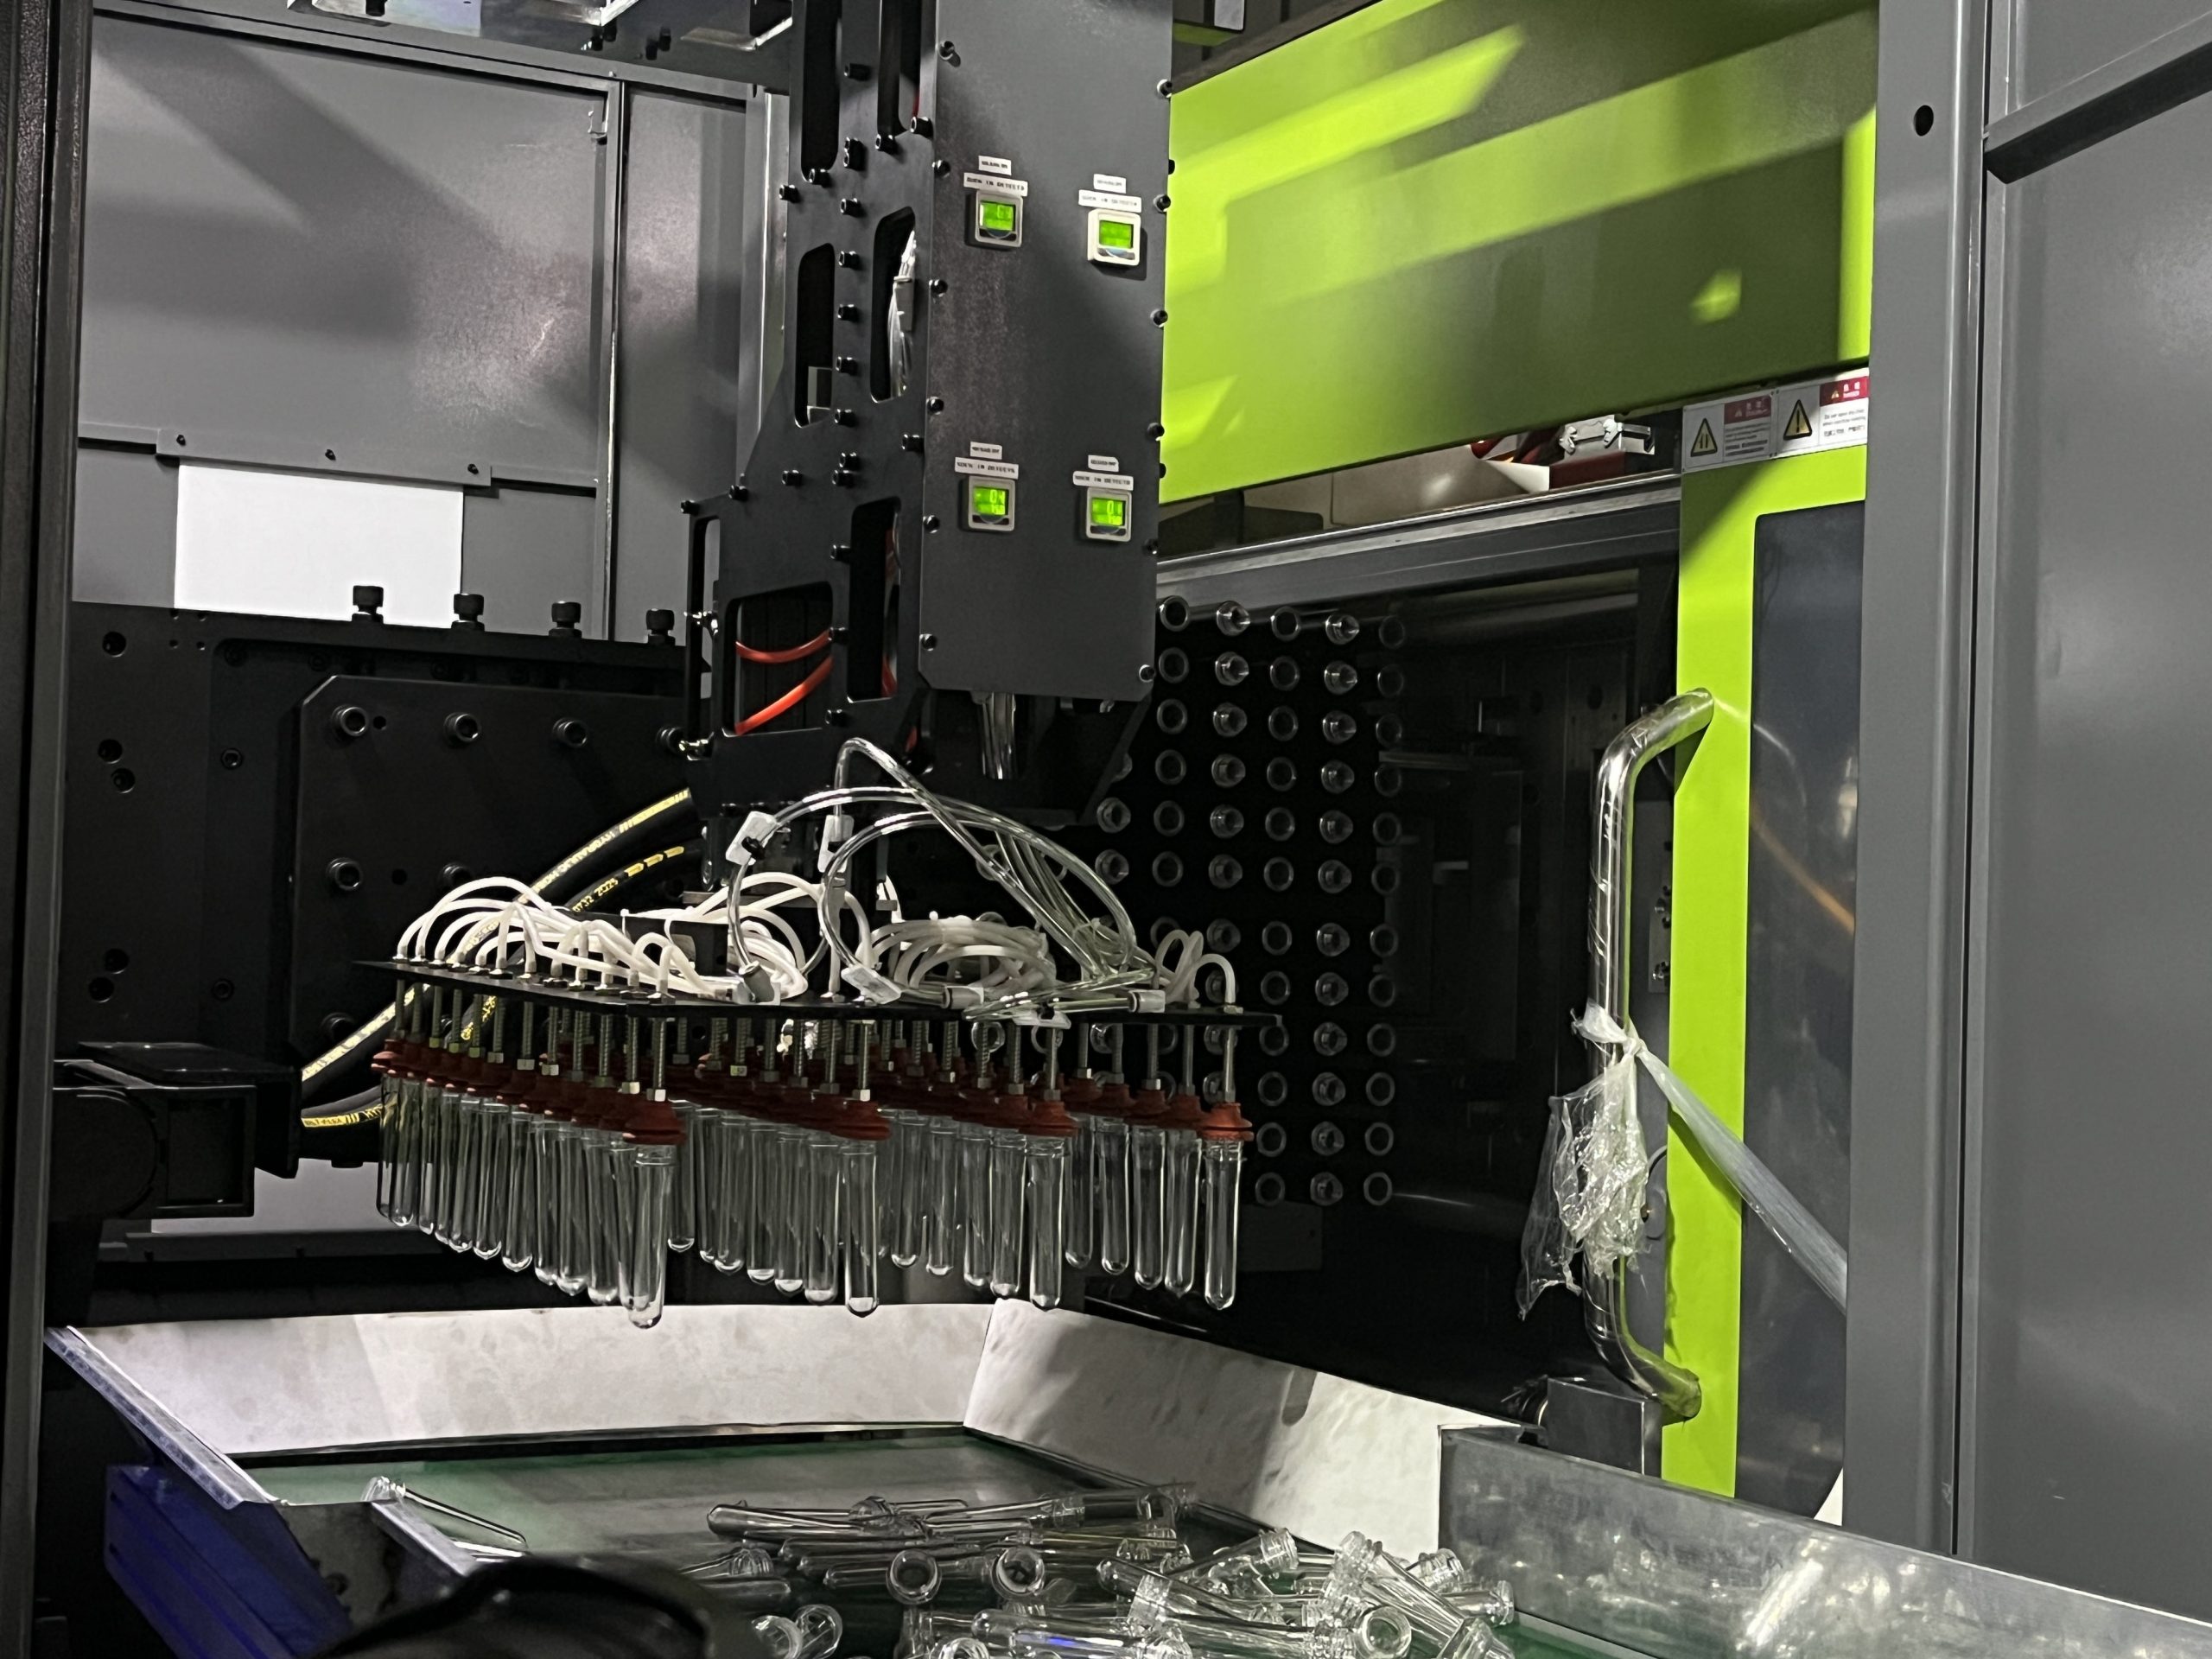
Beyond the machine itself, DKM and SINO MOULD jointly deliver complete PET Preform Production Lines that integrate the preform mold, the DKM-PET III injection molding machine, and a take-out robot into a single pre-commissioned system. Three standardized configurations illustrate the breadth of this offering: a PET 650 machine with 144 cavities and a take-out robot producing an 11g/29mm preform at 12.8 seconds; a PET 450 machine with 72 cavities and a dual-station external cooling robot producing a 12g/28mm preform at 12 seconds; and a PET 350 machine with 48 cavities and a three-station external cooling robot producing a 12g/28mm preform at 16 seconds.
For preforms under 16g, cooling takes place directly on the robot gripper during part removal. For preforms over 16g, robot gripper cooling is combined with multi-station cooling units — an approach designed to allow faster overall molding cycles for heavier preforms without extending the mold’s own cycle time.
On the delivery side, standard 48/72-cavity production lines with standard 28/38mm neck finishes move from order confirmation to qualified shipment in 14 days. Custom, non-standard applications — including special neck finishes, unique bottle designs, or mixed-cavity configurations — are delivered in 5 to 7 weeks. To support this pace, DKM maintains safety stock for PET preform-dedicated machines across the 350T, 450T, 550T, and 650T models, alongside auxiliary equipment, reducing the risk of delay caused by base-machine production queues.
Mold Precision from SINO MOULD
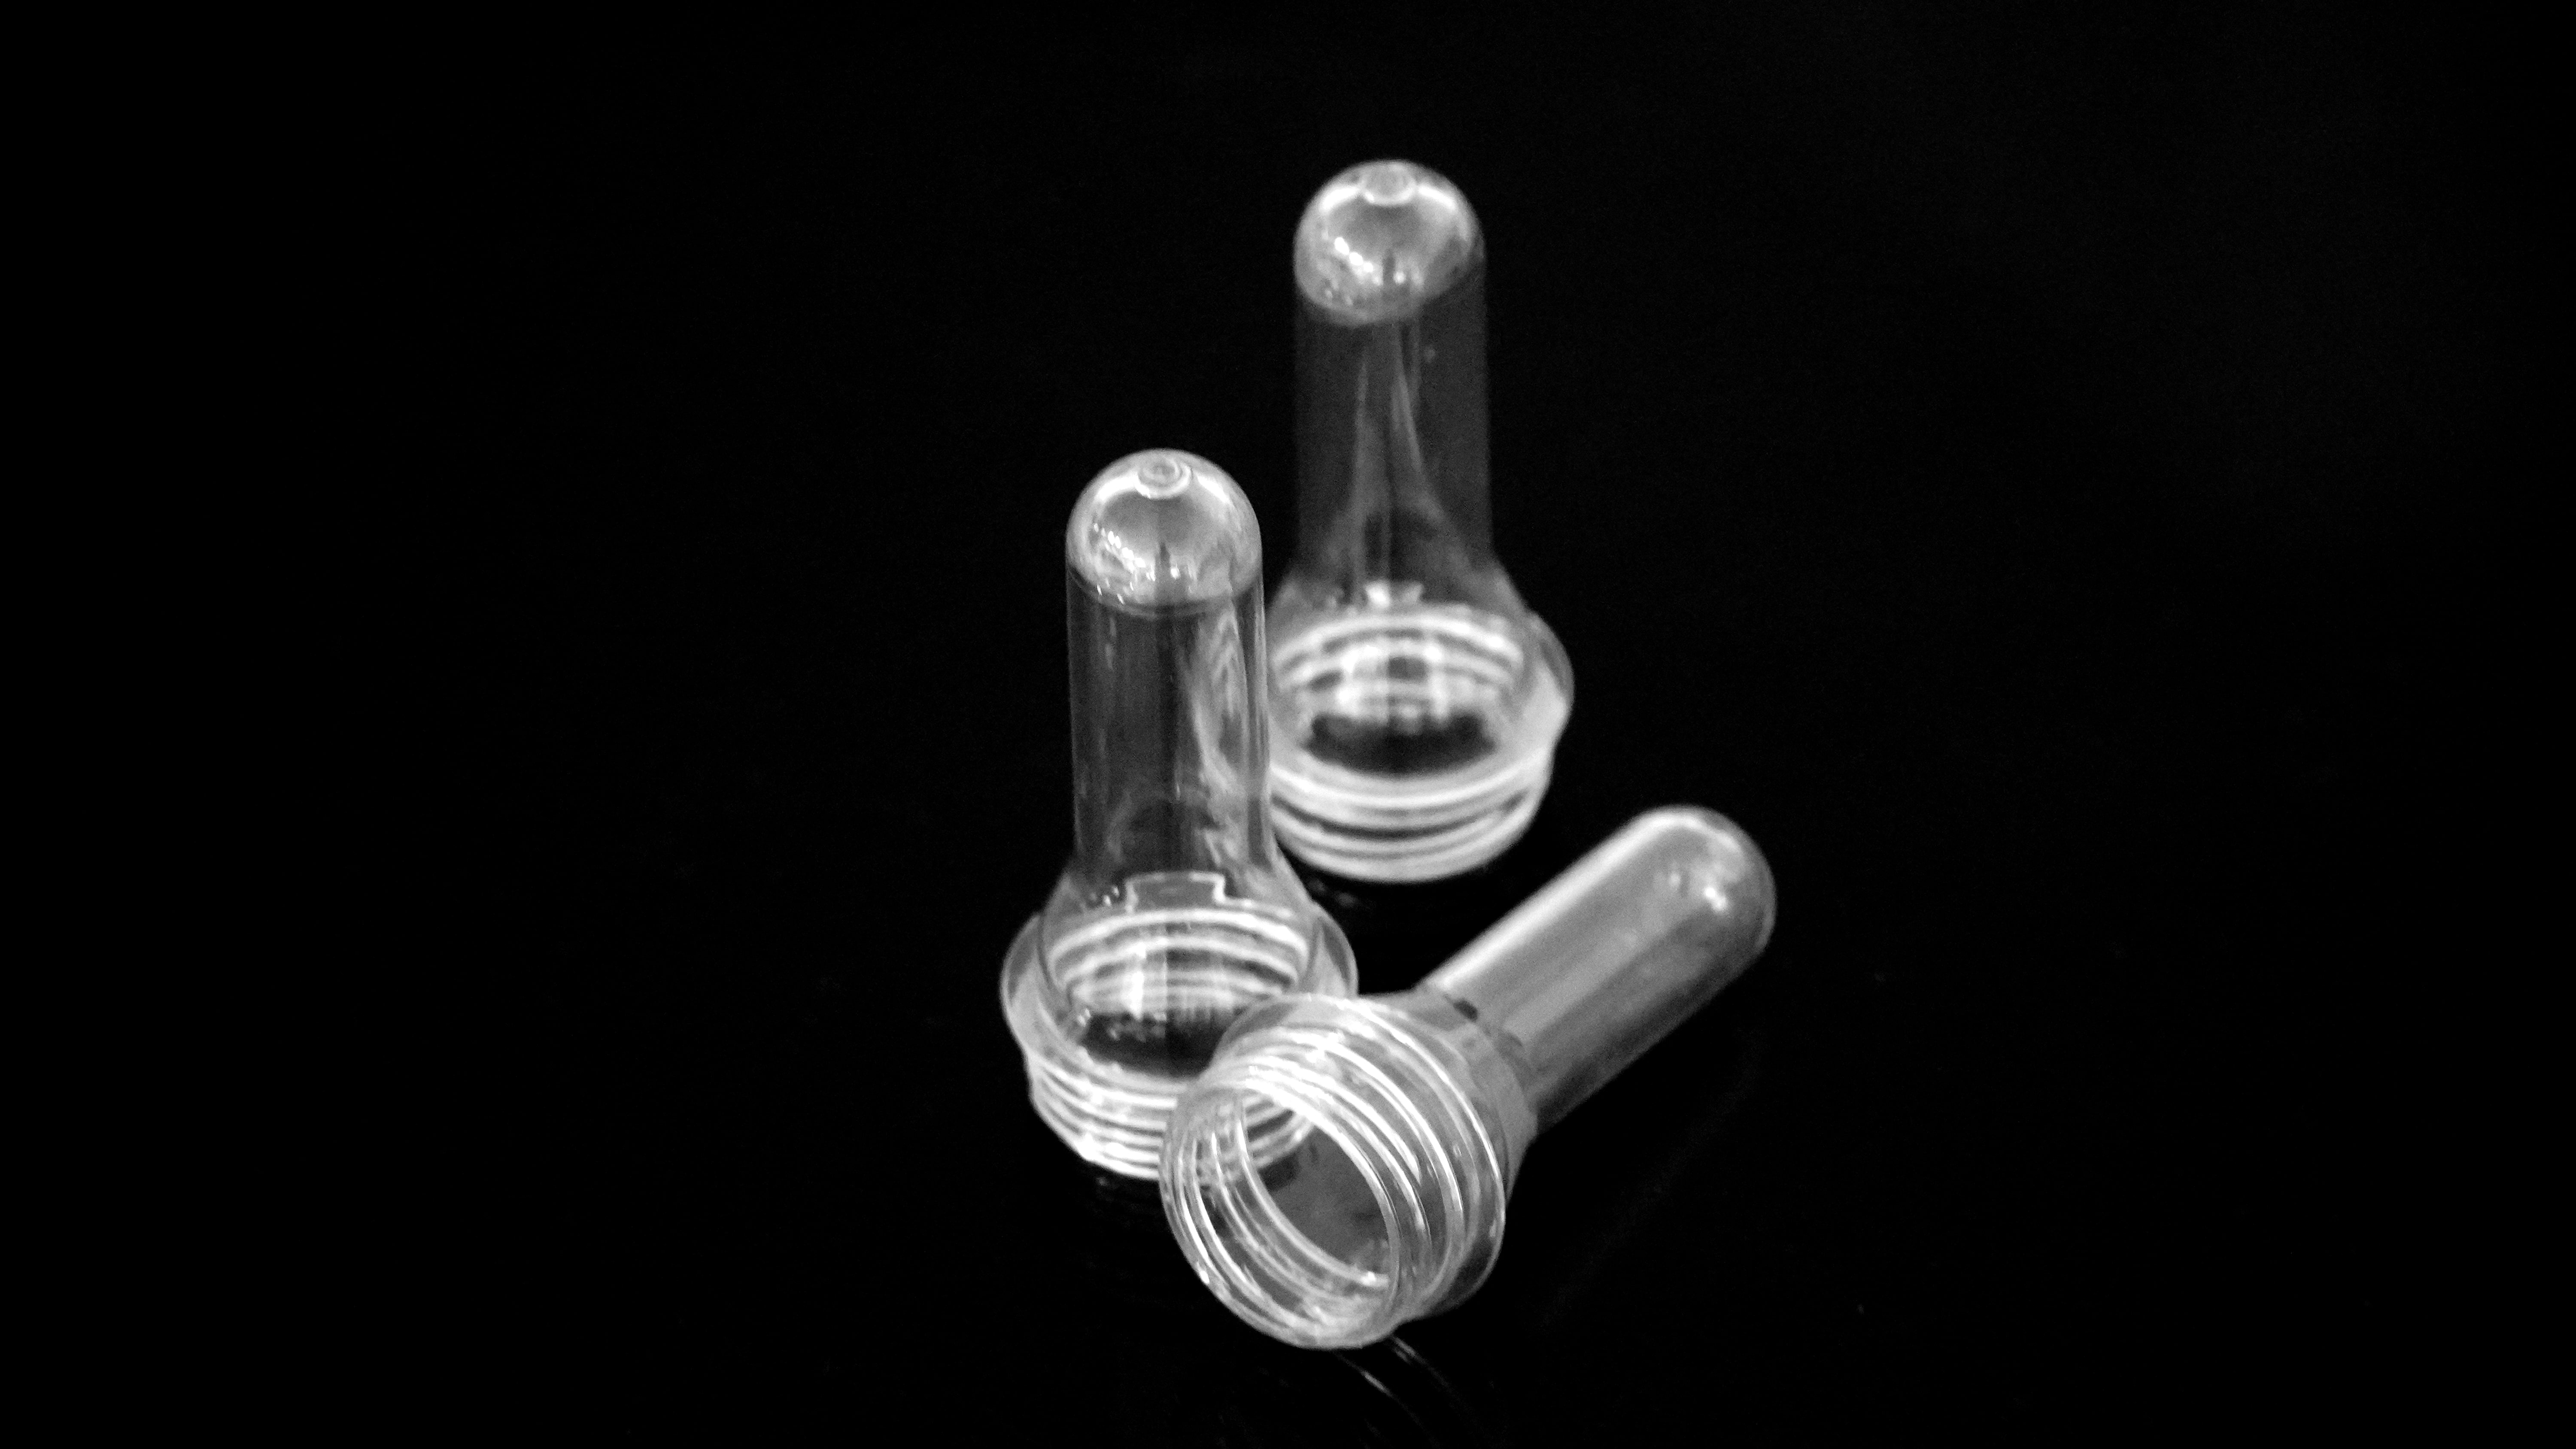
The mold side of the equation is handled by SINO MOULD and its subsidiary SINO-PK, which manufacture PET Bottle Preform Molds across a flexible cavity range from 8 to 144. Key components are produced in Swedish S136 steel (HRC45-48), with the mold base in DIN1.2311 steel, and tolerances held to 0.01mm for uniform wall thickness and concentricity — with select configurations reaching ±0.005mm precision. Standard neck finishes, including PCO 1810 / PCO 1881 and 28mm necks, cover preform weights typically between 12g and 30g. SINO MOULD also offers custom cold-half molds built on existing mold bases to reduce customer investment, alongside fully custom preform molds for non-standard requirements.
Standard 48/72-cavity molds are delivered in 1 to 2 weeks, and these molds carry a 3-year warranty with free spare parts during the warranty period. This combination of precision tolerance, standardized delivery speed, and warranty support reflects over 20 years of multi-cavity preform mold manufacturing expertise, with more than 200 sets of standard PET preform molds delivered worldwide to date.
A Technology Platform Built for Consistency
The underlying capability behind these cycle times and tolerances is not incidental. DKM operates a European R&D team organized by an Italian two-platen machine specialist with 25-plus years of experience, supported by a Technical Office in Italy established in 2018 and a Technology Center in Italy registered in 2023. Over the past ten years, R&D expenditure has accounted for 8% to 10% of the company’s sales revenue — a sustained investment level that underpins continuous process refinement, from the original 2021-era preform cycle benchmarks through to the current 12-second, 26g preform result.
Field-Validated Performance
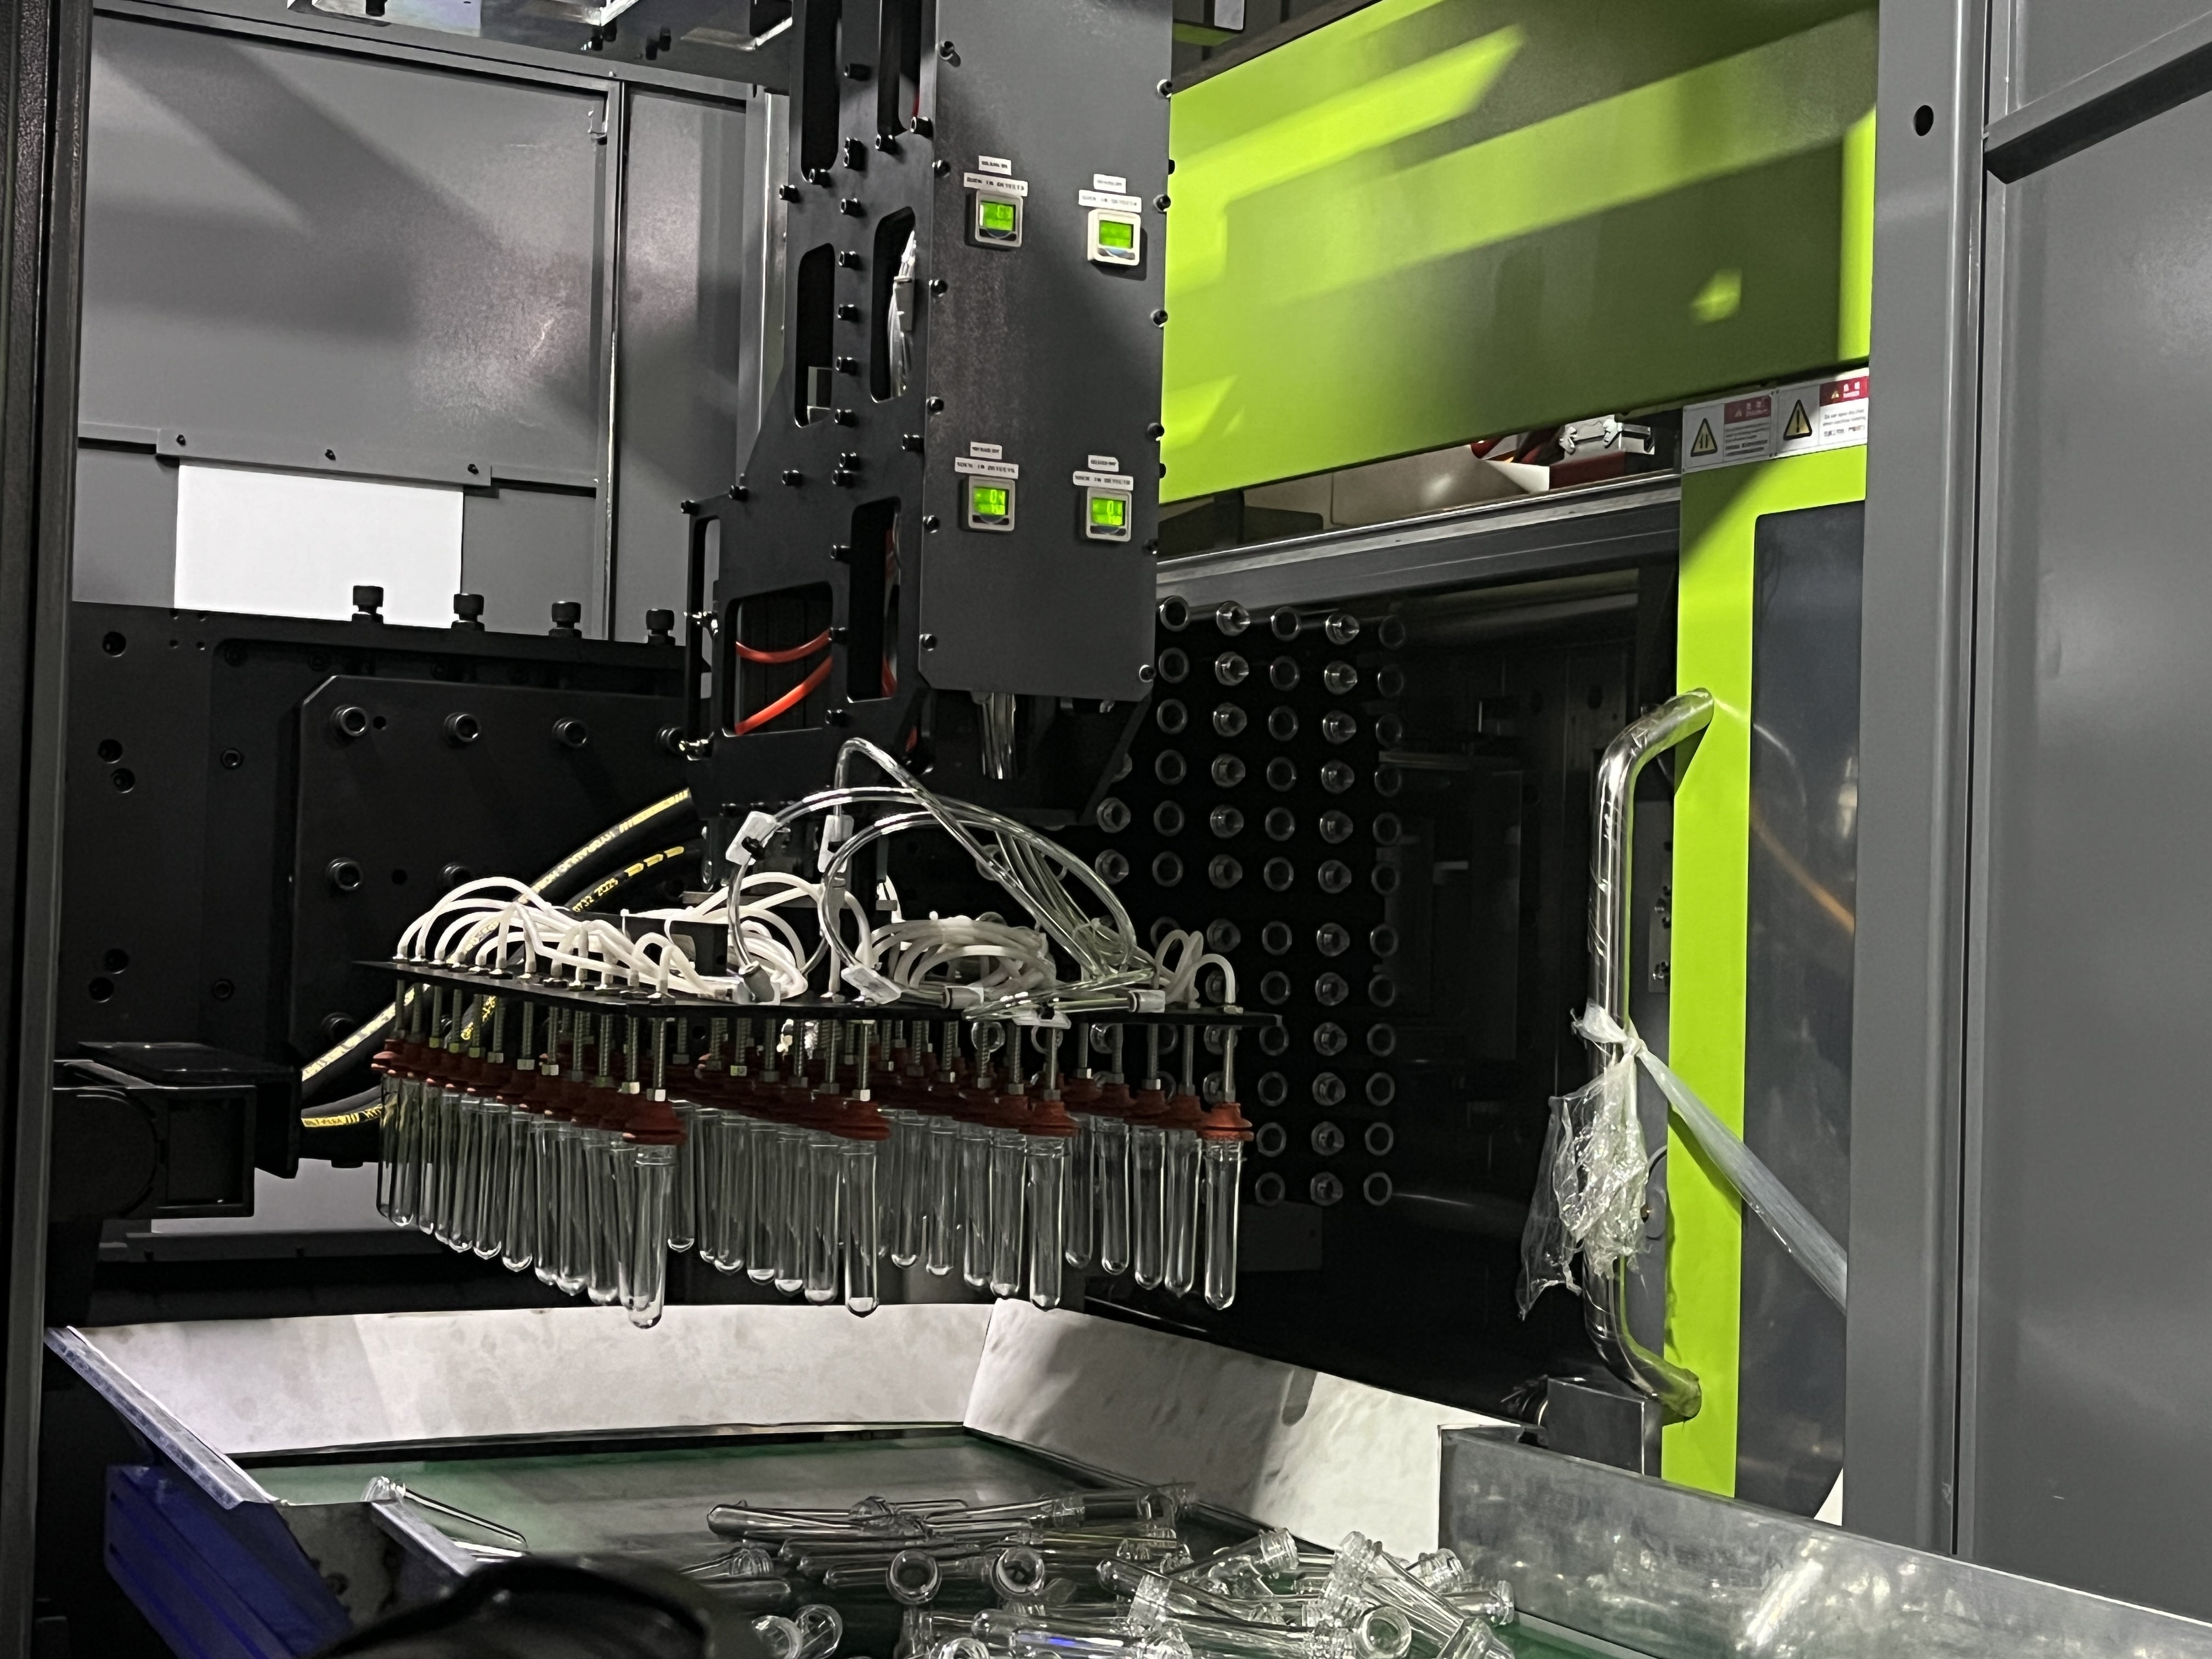
Real-world deployment data reinforces these engineering claims. Two 144-cavity PET preform production lines are currently in operation — one in Iraq and one in Iran — both running under normal production conditions. Customer acceptance test reports have confirmed satisfactory performance, and payment has been settled in full for both projects. Such field validation, combined with an intelligent standardized preform mold workshop scheduled for operational launch, points to a manufacturer whose claims are backed by installed, running equipment rather than laboratory figures alone.
Conclusion
For producers evaluating a PET preform injection molding machine, the relevant questions are rarely about a single specification in isolation — they concern cycle time at scale, tolerance consistency across high cavitation, mold-machine compatibility, and delivery reliability. Across these dimensions, the combined DKM and SINO MOULD offering — spanning the DKM-PET III machine series, SINO MOULD’s precision preform molds, and jointly commissioned turnkey production lines — presents a documented, field-tested answer built on measurable cycle data, defined tolerances, and warranty-backed delivery commitments.
Related products
-
HUB III Bearing Unit Assembly Line
Contact Us● HIGH EFFICIENCY / QUICK CHANGEOVER / FULL AUTOMATION / DATA TRACEABILITY
● LEADING TECHNOLOGY / SIMPLE OPERATION -
INDUSTRIAL DIRECT GAS FIRED TUNNEL OVEN
Contact UsSuitable for a variety of products baking, there are several choices for the type of transporting belt, you can choose the best type based on the products to be baked.
-
Power Conducting Arm
Contact UsPower Conducting Arm is the clamping arm for EAF Electric Arc Furnace Industrial Electrode Arm With Copper Clad Explosion Plate
-
OIL SPRAY MACHINE
Contact UsGuangdong Baimai Equipment Technology Company was established in Dongguan, the city is located in China’s global bay area “Guangdong-Hong Kong-Macao Greater Bay Area”, known for its manufacturing.
Reviews
There are no reviews yet.